<link href="https://fonts.googleapis.com/css2?family=Caveat:wght@500;700&family=JetBrains+Mono:wght@400;500;600&display=swap" rel="stylesheet" /> Skip to main contentEngineering Courses, Mentoring & Jobs | EveryEng
Sour Water System Optimisation banner
Live online Basic

Sour Water System Optimisation

4(1581)
41 enrolled
1468 views
COMPLETED

Tell us and we’ll notify you when the next batch is scheduled.

-
-
1468 views
Team EveryEng
Team EveryEngMechanical Engineering
  • Session recordings included
  • Certificate of completion
Volume pricing for groups of 5+

Why enroll

Enhance your career in chemical engineering with expertise in Sour Water System Optimization! By mastering this specialized skill, you'll become a highly sought-after professional in the oil and gas industry, qualified for roles like Process Engineer, Operations Optimization Specialist, or Environmental Engineer. With expertise in sour water system optimization, you'll minimize environmental impact, reduce operating costs, and improve safety for top companies like Shell, Total, or Saudi Aramco. This course will give you the edge to advance your career, lead process optimization teams, and drive sustainable operations in the energy sector.

What enrolled engineers say

5 verified reviews
  • Feb 25, 2026

    Coming into this course, I had some prior exposure to the subject from refinery operations, mostly dealing with sour water strippers and downstream sulfur recovery units. What was missing was a clear explanation of why oil-in-water emulsions with H2S and NH3 behave so badly in real systems, even when residence time looks fine on paper. The sections on emulsion stability, droplet size distribution, and how it directly drives heat exchanger fouling connected a lot of dots from day-to-day oil & gas troubleshooting. One challenge was keeping up with the balance between theory and field examples, especially around mass transfer limits and separation efficiency. A few case discussions moved fast, but they reflected how issues actually show up during unit upsets. The most practical takeaway was rethinking the “bigger tank fixes everything” mindset. Looking at upstream contamination control, filtration options, and smarter hydraulics is something that can be applied immediately, even without a full revamp. This filled a real knowledge gap between design assumptions and operating reality, and the learnings translate well to other chemical processing systems handling emulsions. I can see this being useful in long-term project work.

    Mamadou Mansour F. Verified
  • Feb 25, 2026

    At first glance, the topics looked familiar, but the depth surprised me. Sour water stripping and hydrocarbon carryover are everyday oil & gas problems, yet the course went beyond the usual “add residence time” thinking. The discussion around stable oil emulsions, especially in H₂S/NH₃-laden water, aligned well with what’s seen in refineries feeding sulfur recovery units, where even small upsets can cascade downstream. One challenge during the course was reconciling the theoretical droplet settling assumptions with real plant data. In practice, heat exchanger fouling and stripper internals plugging don’t behave anywhere near textbook expectations, and that gap was openly addressed. Comparisons with industry-standard API separators versus advanced filtration approaches were useful, particularly for edge cases like high aromatic content or fine solids that keep emulsions stable. From a chemical processing perspective, the linkage between interfacial chemistry, filtration media selection, and system-level energy penalties was handled well. A practical takeaway was rethinking front-end sour water handling instead of over-designing the stripper itself. That has implications for emissions control and long-term operability, not just short-term throughput. Overall, it felt grounded in real engineering practice.

    Siva M. Verified
  • Feb 25, 2026

    This course turned out to be more technical than I anticipated. The discussion around sour water stripper upsets in oil & gas facilities went deeper than the usual residence-time arguments seen in many refineries. The treatment of stable oil-in-water emulsions, especially with concurrent H₂S and NH₃ loading, matched issues seen in both refining and chemical/pharmaceutical wastewater systems, where trace hydrocarbons quietly break downstream units. One challenge was mentally reconciling the idealized separator assumptions with messy field reality. Several edge cases were highlighted—like how exchanger fouling accelerates when emulsions bypass upstream tanks, or how small hydrocarbon slips end up causing disproportionate problems in SRU feed quality. That mirrors what happens in pharma effluent polishing, where minor contaminants can shut down biological systems. Compared to standard industry practice of “bigger tanks and longer holdup,” the course pushed more system-level thinking, including separation technology selection and fouling mitigation strategies. A practical takeaway was re-evaluating where separation actually belongs in the process, rather than overloading the stripper to fix upstream design gaps. The content felt aligned with practical engineering demands.

    Subash N. Verified

Is this course for you?

You should take this if

  • You work in Oil & Gas Upstream or Pharmaceutical & Healthcare
  • You're a Chemical & Process / Geoscience professional
  • You prefer live, instructor-led training with Q&A

You should skip if

  • You need a different specialisation outside Chemical & Process
  • You need fully self-paced, on-demand content

Course details

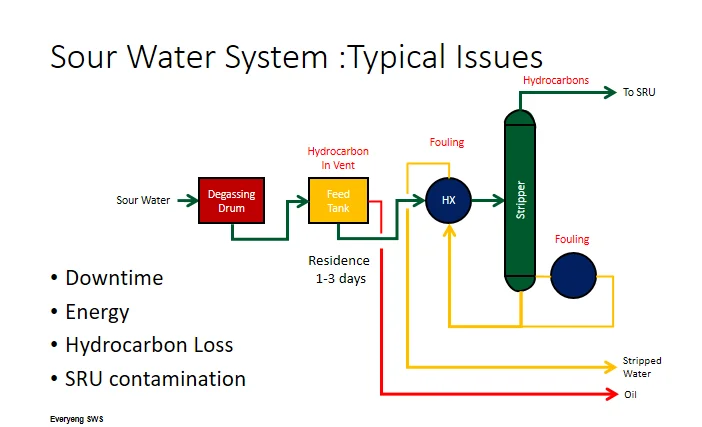
Hydrocarbon contamination of sour water streams feeding sour water strippers is a well-known challenge in the refining and gas processing industry. The source of this challenge is the formation of a stable oil emulsion in an aqueous phase that may contain both H2S and NH3. The typical approach to the problem involves large residence time tanks under the estimation that droplet settling will occur over a long enough time frame. In practice, droplet settling is very slow due to a variety of reasons, and as a result, operators encounter sour water heat exchanger fouling, stripper fouling, hydrocarbon excursions to sulfur recovery units along with other operating challenges. This course will address the relevant issues and identify possible approaches to optimisation, with very significant contribution to energy savings, emission control and improved sulphur recovery goals.   

Trainer - Chemical Engineer from IIT Varanasi and MBA from University of bath UK.


30+ years of experience across manufacturing, design engineering, oil and gas, and speciality chemicals in leadership roles including CXO, General Management, Technical Support, and Business Development positions.


Specialist in Filtration: Advanced Separation Technology for separation of contaminants and process optimization in refineries, gas processing, petrochemicals, upstream-produced water, and power plants.


Other Industries served : Design Engineering, Flame Retardant Additives & Masterbatches, Process Filtration, Petroleum, Refining, Specialty Chemicals, Oil Field Chemicals, Water Treatment & Petrochemicals.

Course suitable for

Key topics covered

Introduction to Hydrocarbon Contamination

Sources and types of hydrocarbon contaminants

Formation of stable oil emulsions

Chemistry of Sour Water Streams

Interaction of H2S and NH3 in aqueous phases

Impact on refining and gas processing operations

Challenges of Droplet Settling

Factors affecting droplet settling rates

Common operational issues caused by slow settling

Optimization Techniques for Sour Water Strippers

Enhancing droplet separation

Design and operational improvements

Energy Efficiency Strategies

Reducing energy consumption in separation processes

Techniques for energy savings in sour water management

Emission Control Measures

Reducing H2S and NH3 emissions

Environmental compliance strategies

Improving Sulfur Recovery

Advanced sulfur recovery techniques

Maximizing efficiency and yield

Case Studies and Practical Examples

Real-world scenarios and solutions

Best practices from leading industry players

Troubleshooting and Problem-Solving

Addressing common operational challenges

Practical tools and techniques for operators

Opportunities that await you!

Career opportunities

Training details

This is a live course that has a scheduled start date.

COMPLETED

-

Questions and Answers

A: That's the most common mistake — treating control checks as a starting point. Internal orientation errors or blocked downcomers don’t show up in a dry loop check, and once you’ve stroked valves and signed ITPs the incentive to reopen the column drops. Mechanical completeness and hydrostatic integrity come first, then instrumentation proves it can control what’s physically correct.

A: That’s the classic slip — forgetting Cp is per unit mass. Once you convert 120 m3/h to about 34 kg/s, the arithmetic lands near 34 × 4.2 × 50, which is well into double‑digit megawatts. Dissolved NH3 and H2S barely move Cp at these concentrations, so discounting them doesn’t rescue an under-sized heater.

A: That’s the confusion — mixing up uniform corrosion with SSC. In wet H2S, crack initiation tracks microstructure and hardness far more than nominal corrosion rate. Keeping welds and base metal below specified hardness cuts the cracking mechanism at its root without forcing a full metallurgy change.

A: That’s where people overthink stripping as evaporation. Almost all the duty is sensible heating of a very large water mass; you’re not boiling it. Convert the flow to about 28 kg/s, multiply through Cp and ΔT, then divide by steam latent heat and you land in the low‑teens tonnes per hour.